A designation such as 304 or 316 does not tell you whether a sheet will survive chlorides, welding, heat, forming, or structural loads. By matching the alloy to its service conditions and writing thickness, tolerance, finish, testing, and delivery requirements into the purchase order, you can compare quotations on performance rather than labels.
Key takeaways
- Choose 304L for welded construction to reduce sensitization risk.
- Specify chloride exposure, temperature, welding method, finish, dimensions, and tolerances.
- Select thickness from load, stiffness, forming, corrosion allowance, and fabrication requirements.
- Check grade, thickness, heat number, surface, and certificates before fabrication.
Match the Grade to Corrosion, Chlorides, and Welding
Use 304 stainless steel sheet for ordinary indoor service, food equipment, and mild atmospheric exposure. Choose 304L for welded construction: its usual 0.030% maximum carbon limits chromium-carbide sensitization during welding, compared with 0.080% for standard 304. It does not automatically improve corrosion resistance.
| Grade | Service-environment fit | Welding and fabrication decision |
|---|---|---|
| 304/304L | General atmospheric, food, and process service; limited chloride exposure | 304L suits welded assemblies; avoid warm, concentrated, stagnant chlorides and tight crevices |
| 316/316L | Better chloride pitting and crevice resistance because molybdenum is typically 2–3% | Choose 316L for welded chloride-service equipment; 316 is not immune to attack |
| 321 | Thermal exposure where carbide stabilization is needed | Confirm the temperature range and welding procedure |
| 310S | High-temperature oxidation and heat service | Select for heat resistance, not as a general chloride upgrade |
| 430 | Dry indoor service, appliances, and decorative work; normally magnetic | Lower chloride resistance and forming capability than austenitic grades |
| 2205 duplex | Higher strength and stronger chloride resistance than 304/316 | Require solution annealing and controlled welding to preserve ferrite–austenite balance |
Use PREN to rank candidates: PREN = %Cr + 3.3(%Mo) + 16(%N). Treat it as a comparison, not a service-life prediction; temperature, chloride concentration, surface condition, inclusions, and crevice geometry still decide failure.
When writing grades for sheets, name ASTM A240 on the purchase order, not only “316L stainless steel sheet.” A magnet cannot verify grade: cold-worked 304 or 316 can become magnetic.
Use Temperature and Metallurgy to Rule Grades In or Out
Choose 321 stainless steel when welded sheet will see prolonged elevated temperatures and you need resistance to sensitization without relying on post-weld stabilization. Choose 310S when oxidation resistance at very high furnace or exhaust temperatures matters more than aqueous corrosion performance; it is not a shortcut for chloride service.
| Grade | When it makes more sense | What rules it out |
|---|---|---|
| 321 stainless steel | Welded parts exposed to sustained heat; titanium stabilization limits carbide sensitization | Strong chloride attack or a need for maximum pitting resistance |
| 310S | High-temperature oxidation, furnace internals, radiant heat and hot gas service | Wet chloride environments, where its high chromium and nickel do not replace molybdenum |
| 430 stainless steel | Magnetic, economical sheet for dry indoor equipment, trim and mildly corrosive service | Severe corrosion, deep forming or demanding welded assemblies |
| Duplex 2205 sheet | Chloride-bearing service needing higher strength and better pitting resistance than 304/316 | Uncontrolled welding, slow cooling or heat treatment that disrupts its ferrite–austenite balance |
Use PREN to rank pitting resistance, not to predict service life. The common formula is PREN = %Cr + 3.3(%Mo) + 16(%N), but temperature, chloride concentration, crevices, inclusions, surface condition and weld metallurgy can overturn the ranking.
Duplex 2205 sheet requires solution-annealed material and controlled welding with a suitable filler. Excessive heat input can reduce toughness and corrosion resistance even when the chemical analysis matches the grade. For any option, identify ASTM A240 on the order rather than buying by a grade number alone.
Turn a Grade Choice into a Complete Purchase Specification
Writing a grade such as 304 or 316 does not tell the supplier enough. Put ASTM A240 and the exact grade, including the L version when welded fabrication matters, on the purchase order. ASTM A480/A480M supplies general requirements for flat-rolled stainless products, but it does not replace your specified dimensions, finish, or acceptance criteria.
State every field that controls fit, fabrication, or service:
- Nominal thickness, permitted thickness deviation, sheet width and length, and their tolerances
- Delivery condition, such as cold-rolled or hot-rolled, plus the required heat-treatment condition
- Surface designation, such as 2B finish, BA finish stainless steel sheet, No. 1, or brushed finish
- Maximum surface roughness value in Ra and the inspection method when cleanability or appearance matters
- Edge condition: mill edge, slit edge, or deburred edge
- Required pickling condition, especially after heat treatment, and whether weld heat tint must be removed
- Mechanical-property requirements, including tensile strength, yield strength, and elongation
- Material test certificate identifying the heat, chemistry, mechanical results, and any testing performed on that heat
Do not treat passivation as a substitute for grade selection or pickling. If required, name ASTM A967/A967M and the treatment—nitric acid, citric acid, or electrochemical—because each addresses free iron and surface cleanliness, not chloride resistance. State the inspection documents and rejection limits before production starts.
Choose Thickness for Load, Stiffness, and Fabrication Reality
A sheet that carries a load across a long span needs more thickness for stiffness, even when its calculated strength is adequate. Size for the load case, unsupported span, pressure, deflection limit, and attachment method—not for weight alone.
| Driver | Effect on the order thickness | What to check |
|---|---|---|
| Load and span | Greater load or span increases bending stress and deflection | Support spacing, concentrated loads, allowable deflection, and buckling |
| Pressure | Internal pressure demands code-based wall thickness and reinforcement | Governing design code, such as ASME BPVC Section VIII, plus openings and weld joints |
| Corrosion allowance | Consumed metal must be added to the required service wall | Expected loss over the design life, including pitting or crevice attack |
| Forming | Bending, rolling, and deep drawing can thin corners or introduce cracking | Bend radius, grain direction, forming strain, and post-forming measurements |
| Mill tolerance | The nominal thickness is not necessarily the minimum delivered thickness | ASTM A240 and ASTM A480/A480M tolerance tables, product form, width, and rolling route |
Your purchase specification must state the stainless steel sheet thickness as a nominal thickness and identify the permitted tolerance. A negative thickness tolerance means the actual measured thickness can fall below nominal; design the minimum acceptable wall before adding corrosion allowance, and do not assume the quotation’s nominal thickness is a guaranteed minimum.
Forming reality can change the choice. Order a thicker starting gauge when bending or drawing will reduce the wall, and confirm the finished geometry with measurements. Specify ASTM A240 and the required ASTM A480/A480M tolerance or a tighter agreed tolerance; cold-rolled material improves dimensional control but does not replace structural calculation.
Verify the Delivered Sheet Before It Enters Fabrication
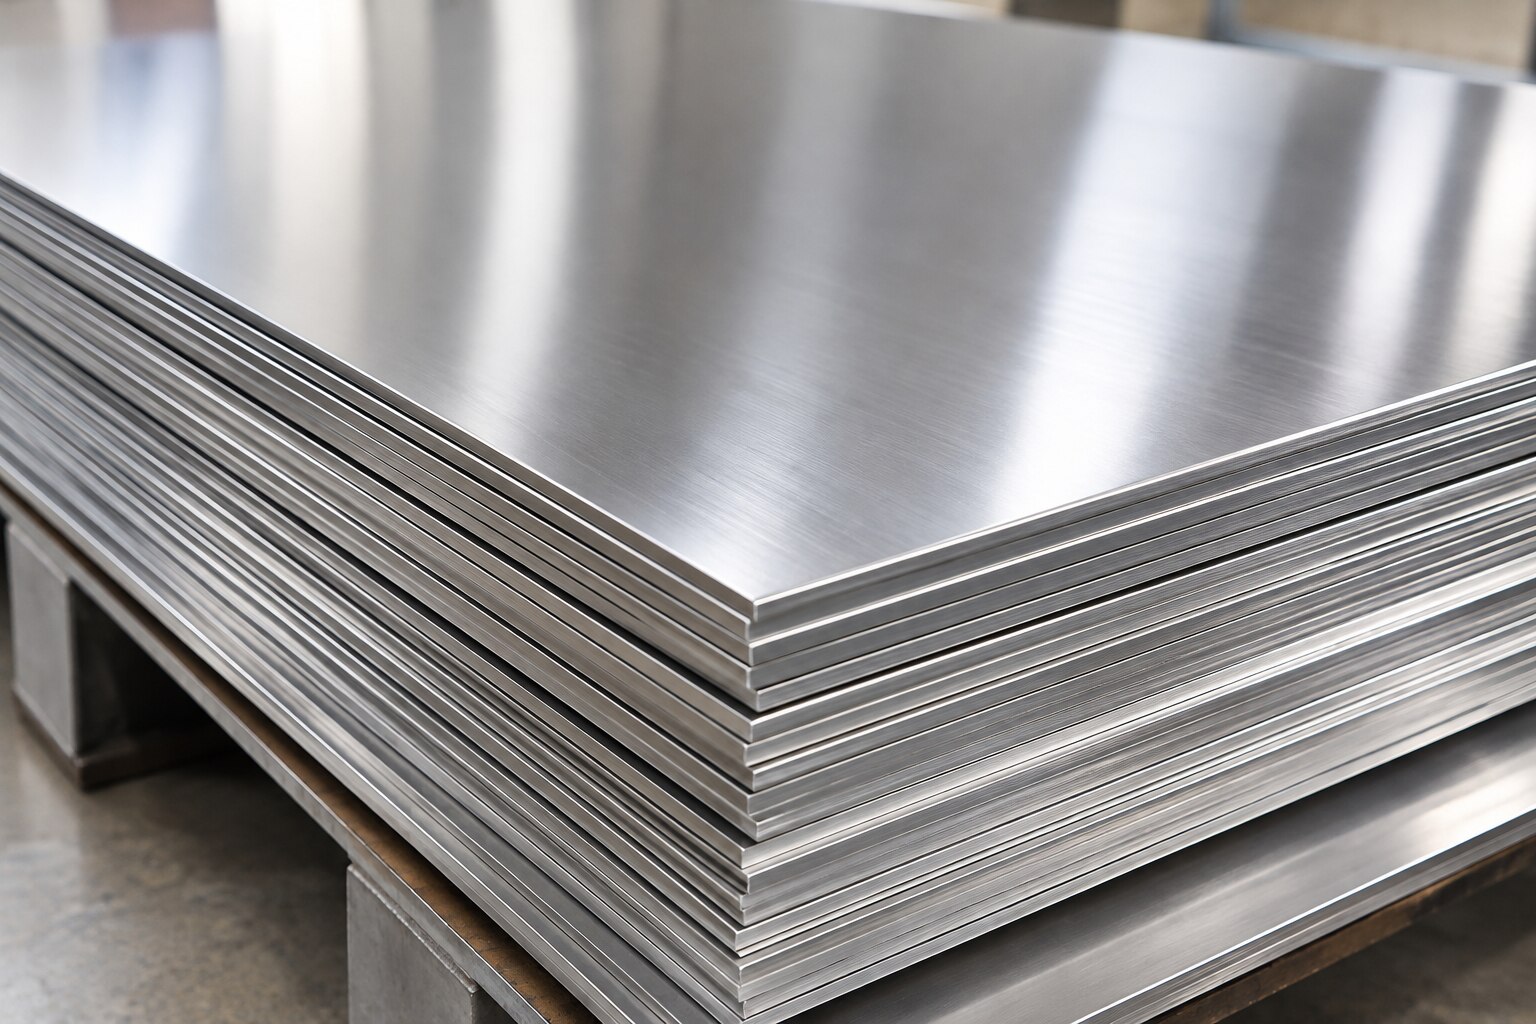
Do not release the sheet to fabrication until its heat number, certificate, dimensions, and surface condition agree with the purchase order. A stainless steel sheet inspection should trace each bundle to the test report, not rely on a bright finish or a grade stamped on the packaging.
- Match the marking to the EN 10204 3.1 certificate: heat number, grade, chemistry, tensile results, yield strength, elongation, product form, and quantity.
- Require an EN 10204 3.2 certificate when your contract or pressure-equipment procedure demands independent inspection or purchaser verification. State this before production, not after delivery.
- Measure thickness with a calibrated micrometer at several positions, then check width, length, squareness, and flatness against ASTM A480/A480M tolerances.
- Inspect both faces for pits, dents, laminations, deep scratches, rust staining, embedded iron, and weld-like heat tint. A polished surface does not prove clean handling.
- Ask whether ASTM A240 applies, which finish and delivery condition were supplied, and whether the reported tests came from the actual heat.
- If passivation is specified, request the treatment record for ASTM A967 passivation; it removes free iron but does not replace pickling for weld heat tint.
| Document | Confirm | Question for the supplier |
|---|---|---|
| EN 10204 3.1 | Manufacturer’s results | Which heat does this report cover? |
| EN 10204 3.2 | Independent or purchaser validation | Who witnessed the inspection? |
| ASTM A480/A240 | Product and dimensional rules | Which tolerances and finish were supplied? |
If SMD Impex is coordinating sheet with tube or pipe fabrication, keep one heat-number trail across every related item. Reject mismatched markings before cutting.
Frequently asked questions
When should you choose 304L instead of 304 stainless steel sheet?
Choose 304L for welded construction when its 0.030% maximum carbon reduces chromium-carbide sensitization during welding. It does not automatically provide higher corrosion resistance than 304.
How do chlorides affect stainless steel grade selection?
Chlorides increase the risk of pitting and crevice corrosion. Assess concentration, temperature, wetting time, deposits, and cleaning conditions before selecting a grade; 316 or a higher-alloy grade can be more suitable than 304 in severe chloride service.
What information belongs in a stainless steel sheet purchase specification?
State the grade and standard, thickness and tolerances, sheet dimensions, surface finish, edge condition, quantity, certificate requirements, heat or lot traceability, inspection requirements, and welding or forming needs.
How do you choose stainless steel sheet thickness?
Base thickness on load, span, stiffness, buckling, corrosion allowance, forming limits, weld distortion, support spacing, and the available fabrication process rather than nominal thickness alone.
What should you verify when stainless steel sheets arrive?
Compare the marking and packing list with the order, then check grade, thickness, dimensions, surface condition, heat number, quantity, and the mill test certificate before releasing sheets to fabrication.